How an Extrusion Blow Molding Machine Factory Manages Customized Extrusion Head Designs
How an Extrusion Blow Molding Machine Factory Manages Customized Extrusion Head Designs
Customized extrusion head design is a critical capability for extrusion blow molding machine factories. It determines parison quality, wall thickness, cycle time, material usage, and overall production efficiency. This article examined how Guangdong Leshan Intelligent Equipment Corp., Ltd., referred to as Leshan, manages custom extrusion head projects from start to finish. The process begins with requirement gathering and application analysis, followed by material and rheology assessment. Engineers then create designs using CAD and simulation, focusing on flow channels, die gap, mandrel, spider legs, heating zones, and parison control. Collaborative review with the customer ensures the head matches the blow mold, machine, and production goals. Precision manufacturing maintains tolerances within plus or minus 0.05 mm. Assembly, testing, and validation confirm performance before shipment. Installation, commissioning, and training help customers achieve smooth start-up. Lifecycle support and continuous improvement keep the head reliable over time. Leshan integrates extrusion heads with blow molding systems, centralized feeding, and auxiliary equipment such as crushers, mixers, chillers, and conveyors. Its solutions support single-layer, double-layer, and multi-layer blow molding, capacities from 100 mL to 10 L, and quick mold changes under 10 minutes. Case studies include a beverage line producing over 50 million bottles annually with zero mold failure for two years, a multi-layer PET cosmetics line that increased efficiency by 30 percent, and an industrial container line running 24/7 for 18 months with ROI in under 12 months. Quality systems meet ISO 9001 and CE standards, with defect rates under 0.5 percent. By combining expertise, customization, durability, and customer-centric support, Leshan demonstrates how a factory can manage customized extrusion head designs as a strategic advantage.
In the world of plastic manufacturing, extrusion blow molding is a cornerstone technology for producing hollow plastic parts such as bottles, containers, jars, and industrial tanks. At the center of this process is the extrusion head, often called the die head. The extrusion head determines how molten plastic is distributed, shaped, and formed into a parison before it is captured by a mold and inflated. For factories that build blow molding machines, managing customized extrusion head designs is one of the most complex and valuable capabilities they can offer. It requires a blend of mechanical engineering, polymer science, precision manufacturing, project management, and customer collaboration. This article examines how an extrusion blow molding machine factory, using the example of Guangdong Leshan Intelligent Equipment Corp., Ltd., hereinafter referred to as Leshan, manages customized extrusion head designs from initial inquiry to long-term support.
Leshan specializes in turnkey solutions that simplify production and enhance efficiency. Its expertise covers a wide range of plastic molding technologies, ensuring seamless operation, increased output, and reduced operational costs. The company offers blow molding systems, centralized feeding systems, fully automatic systems, customized project solutions, and comprehensive support. Each of these areas interacts with extrusion head design. A customized extrusion head cannot be developed in isolation. It must match the blow molding machine, the mold, the feeding system, the auxiliary equipment, and the final product requirements. This integrated approach is what allows a factory like Leshan to deliver reliable, high-performance extrusion heads for demanding applications.
Understanding the Extrusion Head in Blow Molding
The extrusion head is the component that receives molten plastic from the extruder and shapes it into a tubular parison. The parison is then clamped inside a mold, inflated with air, cooled, and ejected as a finished product. The extrusion head controls critical variables such as material distribution, wall thickness, melt pressure, melt temperature, and parison dimensions. In single-layer blow molding, the extrusion head may be relatively simple. In multi-layer blow molding, the extrusion head becomes a complex assembly with multiple flow channels, separate manifolds, and precise layer distribution. For customized projects, the extrusion head must be designed around the customer's bottle shape, capacity, resin type, production speed, and quality standards.
Factories that build blow molding machines must manage many types of extrusion heads. These include continuous extrusion heads, accumulator heads, multi-parison heads, and co-extrusion heads. Each type has different design rules. For example, an accumulator head stores molten plastic and pushes it out rapidly to form a large parison for industrial containers. A continuous head produces a steady parison for smaller bottles and high-speed lines. A multi-parison head produces several parisons at once to increase output. A co-extrusion head combines multiple materials into a single parison with layers for barrier properties, color, or recycled content. Managing customized designs means understanding how these categories overlap and how each customer's application fits into them.

Why Custom Extrusion Head Designs Are Essential
No two blow molding projects are exactly alike. A dairy bottle, a cosmetic jar, a chemical container, and a pharmaceutical bottle all have different requirements. The resin may be PET, PP, PE, HDPE, LDPE, or a blend. The bottle may need a specific wall thickness for strength, a particular neck finish for a cap, a handle for ergonomics, or a multilayer structure for barrier performance. The production speed may range from a few hundred bottles per hour to several thousand per station. The mold may be a single-cavity or multi-cavity design. All these factors influence the extrusion head.
A standard extrusion head may work for a narrow range of products, but it often fails when the customer needs something unique. Customization allows the factory to optimize flow channels, die gap, mandrel shape, and heating zones. It allows the customer to achieve uniform wall thickness, reduce scrap, shorten cycle time, and improve bottle quality. It also allows the factory to support quick mold changes, multi-layer structures, and special materials. Without custom extrusion head design, many high-value packaging projects would be impossible or unprofitable.
- Product variety: Capacities from 100 mL to 10 L and beyond require different parison sizes and die geometries.
- Material diversity: PET, PP, PE, and engineering resins have different melt strengths and flow behaviors.
- Layer structures: Multi-layer bottles need separate channels and precise layer thickness control.
- Production speed: High-speed lines need balanced flow and rapid parison formation.
- Quality standards: Aesthetic, barrier, and mechanical requirements demand tight tolerances.
The Role of a Specialized Factory Such as Leshan
Leshan has over 15 years of experience in designing and manufacturing blow molding systems. This experience matters because extrusion head design is not only a theoretical exercise. It requires knowledge of how real machines behave in real factories. The company has worked with beverage producers, cosmetic brands, household product manufacturers, and industrial container makers. It has seen how small changes in die design affect wall thickness, cycle time, and defect rates. It has learned how to balance standardization with customization. This accumulated expertise allows Leshan to approach each extrusion head project with a structured methodology.
The company is more than just a supplier. It positions itself as a partner in success. Its proven expertise, tailored solutions, reliability, customer-centric approach, and innovative technology are the foundation of its extrusion head management process. When a customer requests a customized extrusion head, Leshan does not simply copy an existing design. It analyzes the application, evaluates the material, simulates the flow, manufactures the components, tests the assembly, and supports the installation. This end-to-end approach reduces risk and ensures that the final extrusion head performs as expected.

Step 1: Requirement Gathering and Application Analysis
The first step in managing a customized extrusion head design is requirement gathering. Leshan's engineers begin by asking detailed questions about the customer's product and production goals. What is the bottle or container capacity? What is the neck diameter? What is the body shape? What is the desired wall thickness? What resin will be used? Will the product be single-layer, double-layer, or multi-layer? What is the target output per hour? What is the available floor space? What are the downstream operations, such as filling, labeling, and packing? These questions form the basis of the extrusion head specification.
Application analysis also includes a review of the existing production environment. If the customer already has a blow molding machine, the new extrusion head must be compatible with its extruder, clamping unit, hydraulic system, and control system. If the customer is purchasing a complete line, the extrusion head must be integrated with the blow molding machine, the central feeding system, the chiller, the crusher, the mixer, and the conveyor belt. Leshan's engineers document all these requirements in a project brief. This brief becomes the reference point for every subsequent design decision.
Key Questions During Requirement Gathering
- What is the product type and application?
- What is the required capacity range?
- What material or materials will be used?
- What is the target production speed?
- What are the quality and tolerance requirements?
- What are the available utilities and space constraints?
- What is the expected maintenance schedule?
- What is the budget and timeline?
Step 2: Material and Rheology Assessment
Once the requirements are clear, the factory assesses the material. Different plastics behave differently when melted. PET, PP, PE, and other resins have unique viscosity curves, melt strengths, and die swell characteristics. Die swell is the expansion of the parison as it exits the die. If the extrusion head is not designed for the material's die swell, the parison may be too thick, too thin, or inconsistent. The engineers at Leshan study the material data sheets and, when necessary, request samples for testing. They consider melt flow index, thermal stability, shear sensitivity, and cooling behavior.
Material assessment also affects the choice of metallurgy and surface finish. Some resins are corrosive or abrasive. Some require special coatings to prevent sticking. Some multi-layer structures need compatible tie layers. The extrusion head must be made from high-precision steel that can withstand high temperature and pressure. Leshan uses high-grade materials to ensure stable dimensions and long lifespan. The flow channels are polished to reduce friction and prevent material degradation. Heating zones are designed to maintain uniform temperature across the entire head.
Material Factors That Influence Extrusion Head Design
- Viscosity: Determines flow channel dimensions and pressure drop.
- Die swell: Affects die gap and parison dimensions.
- Thermal stability: Influences residence time and heating control.
- Shear sensitivity: Requires balanced flow to avoid degradation.
- Corrosiveness: Dictates steel grade and surface treatment.
- Cooling rate: Affects cycle time and mold design.
Step 3: Design Engineering and Simulation
With the requirements and material data in hand, Leshan's design engineers create a custom extrusion head concept. They use computer-aided design to model the flow channels, mandrel, die ring, spider legs, and heating elements. They pay close attention to the melt flow path. Sharp corners, dead spots, and unbalanced channels can cause material stagnation, uneven wall thickness, and defects. The goal is to create a streamlined path that delivers molten plastic uniformly to the die exit.
Simulation plays a critical role. Computational fluid dynamics helps the engineers predict how the polymer will flow through the head. They can evaluate pressure distribution, velocity profiles, temperature uniformity, and shear stress. This virtual testing reduces the need for physical prototypes and shortens the development cycle. It also allows the factory to optimize the design before any metal is cut. For multi-layer heads, simulation is even more important because each layer must maintain its integrity and thickness.
Leshan's precision engineering ensures mold tolerance within plus or minus 0.05 mm, which guarantees consistent bottle quality. This level of precision is not accidental. It comes from careful design, advanced machining, and rigorous quality control. During the design phase, engineers also consider manufacturability. They choose dimensions that can be machined accurately, assembled easily, and maintained efficiently. They use modular design principles where possible, so that future changes can be made without replacing the entire head.
Core Design Elements of a Custom Extrusion Head
- Die gap: The opening that forms the parison thickness.
- Mandrel: The inner component that shapes the inside of the parison.
- Spider legs: Supports that hold the mandrel and affect flow lines.
- Flow channels: Passages that distribute melt evenly.
- Heating zones: Independent temperature control for each section.
- Parison controller: Adjusts wall thickness during extrusion.
- Accumulator: Stores melt for large parisons in industrial applications.
Step 4: Collaborative Review and Approval
Custom extrusion head design is a collaborative process. Leshan's engineers present the design to the customer for review. They explain how the head will perform, what output can be expected, and how it will integrate with the rest of the line. The customer may have concerns about bottle appearance, cycle time, or material usage. The engineers listen, adapt, and revise the design as needed. This customer-centric approach ensures that the final product meets the customer's unique production needs.
During the review, the team may also discuss the blow mold. The extrusion head and the blow mold must work together. The parison size must match the mold cavity. The neck finish must align with the mold's neck insert. The wall thickness distribution must suit the mold's cooling channels. Leshan offers blow molds that are compatible with single-layer, double-layer, or multi-layer extrusion blow molding machines. These molds are made of high-precision steel to ensure stable dimensions and accurate bottle openings. They are customizable in capacity, shape, and wall thickness, and they support quick mold changes. By considering the mold and the head together, the factory avoids integration problems later.
Step 5: Precision Manufacturing and Machining
After the design is approved, manufacturing begins. The extrusion head is made from high-grade steel. Each component is machined to exact specifications. CNC machining centers, grinding machines, and polishing equipment are used to achieve the required tolerances. The flow channels are polished to a mirror-like finish to minimize friction and prevent material build-up. The die and mandrel are matched precisely to ensure uniform wall thickness. Heating elements and thermocouples are installed and wired according to the design.
Quality control is embedded in every step. Inspectors measure dimensions, check surface finishes, and verify material certificates. The factory uses advanced metrology to confirm that tolerances are within plus or minus 0.05 mm. This precision is essential for consistent bottle quality. If the die gap is too large or too small, the parison will be wrong. If the flow channels are unbalanced, some bottles will be thick and others thin. If the heating zones are inaccurate, the melt temperature will vary, causing weak seams or poor surface finish. Leshan's manufacturing team understands these relationships and works to eliminate variation.
Manufacturing Quality Checkpoints
- Raw material verification and certification.
- CNC machining accuracy checks.
- Flow channel polishing and inspection.
- Die and mandrel dimensional matching.
- Heating zone resistance and insulation tests.
- Assembly fit and alignment checks.
- Pressure and leak testing.
- Final performance validation.
Step 6: Assembly, Testing, and Validation
Once the components are manufactured, the extrusion head is assembled. The assembly process requires skilled technicians who understand the importance of alignment, torque, and sealing. Every bolt, gasket, and heater is installed according to the design. The head is then mounted on a test stand or a blow molding machine. The factory runs trials with the actual material or a representative material. Engineers measure parison dimensions, wall thickness, output rate, and energy consumption. They check for leaks, uneven flow, and temperature variations.
Testing is not only about the extrusion head. It is also about integration. The head must work with the blow molding machine, the central feeding system, and the auxiliary equipment. Leshan's centralized feeding systems control the conveying and drying of plastic materials, ensuring stable temperature and reducing manual labor. They can connect multiple extruders or blow molding machines for centralized management. During testing, the team verifies that the feeding system delivers material consistently to the extruder. They also check the chiller, crusher, mixer, and conveyor belt. If any issue arises, it is addressed before shipment.
Validation includes bottle testing. The factory produces sample bottles and inspects them for wall thickness, weight, dimensions, appearance, and strength. Leak testing and visual inspection systems are used to guarantee defect rates under 0.5 percent. If the bottles meet the customer's specifications, the extrusion head is approved for delivery. If not, the engineers make adjustments and repeat the tests. This iterative process ensures that the customized extrusion head performs reliably in production.
Step 7: Installation, Commissioning, and Training
Shipping a custom extrusion head is only the beginning. Leshan provides comprehensive support, including installation and commissioning. Field engineers travel to the customer's factory to mount the head, connect utilities, and integrate it with the existing line. They calibrate temperature controllers, adjust parison controllers, and fine-tune the die gap. They run production trials and optimize settings for the customer's specific product. This hands-on support reduces downtime and ensures a smooth start-up.
Training is another critical part of the process. The customer's operators and maintenance staff learn how to start, stop, and adjust the extrusion head. They learn how to change molds quickly, often in under 10 minutes with Leshan's quick mold-change system. They learn how to troubleshoot common issues such as uneven wall thickness, parison curling, and heater failure. They also learn preventive maintenance procedures. This knowledge empowers the customer to run the line efficiently and extend the life of the extrusion head.
Commissioning Checklist
- Verify mechanical alignment and mounting.
- Check electrical connections and heating zones.
- Confirm material feed and drying settings.
- Adjust die gap and parison controller.
- Run trial production and inspect bottles.
- Optimize cycle time and wall thickness.
- Train operators and maintenance staff.
- Document final settings and parameters.
Step 8: Lifecycle Support and Continuous Improvement
After commissioning, Leshan continues to support the customer throughout the lifecycle of the extrusion head. The company offers technical consulting, system integration, maintenance, and upgrades. If the customer wants to produce a new bottle size or switch to a different material, Leshan can modify the extrusion head or supply new components. If production conditions change, the company can help optimize settings. This long-term partnership is a key reason why businesses choose Leshan.
Continuous improvement is built into the process. The factory collects feedback from the field, analyzes performance data, and incorporates lessons into future designs. If a particular flow channel design works well, it may become a standard module. If a heating zone configuration reduces energy consumption, it may be adopted across projects. This cycle of learning and improvement keeps Leshan ahead of industry advancements. It also ensures that customized extrusion heads become more reliable, efficient, and durable over time.
Key Design Parameters in Custom Extrusion Heads
Managing customized extrusion head designs requires mastery of many parameters. Each parameter affects the final product and the production process. The table below summarizes the most important ones. Although the table is presented as a list for clarity, it reflects the detailed specifications that Leshan's engineers manage daily.
- Die diameter: Determines the outer diameter of the parison.
- Mandrel diameter: Determines the inner diameter of the parison.
- Die gap: Controls parison thickness and wall distribution.
- Land length: Affects pressure drop and die swell.
- Flow channel geometry: Ensures balanced melt distribution.
- Spider leg design: Minimizes flow lines and weld lines.
- Heating zones: Maintains uniform melt temperature.
- Temperature control: Prevents degradation and improves surface finish.
- Pressure rating: Ensures safe operation at high output.
- Material compatibility: Matches steel and coatings to the resin.
- Parison controller: Adjusts wall thickness for complex shapes.
- Accumulator capacity: Supports large industrial parisons.
- Layer distribution: Controls multi-layer thickness and adhesion.
- Cooling integration: Works with mold cooling for faster cycles.
- Maintenance access: Allows cleaning and replacement without long downtime.
Managing Multilayer and Co-Extrusion Complexity
Multi-layer extrusion blow molding is one of the most demanding areas of customization. In a multi-layer head, two or more extruders feed different materials into a single die. The materials may include virgin resin, recycled resin, adhesive tie layers, and barrier resins. The extrusion head must keep these layers separate until they reach the die exit. It must also control the thickness of each layer. If the layers mix or become uneven, the bottle may fail barrier tests, look unattractive, or have weak mechanical properties.
Leshan supports custom bottle designs, capacities from 100 mL to 10 L, and multi-layer PET and PP blow molding. For a multi-layer project, the engineers design separate manifolds and flow channels for each material. They use simulation to balance the flow and predict layer thickness. They select materials and surface finishes that prevent cross-contamination. They also design the heating system to maintain the different processing temperatures required by each resin. During testing, they measure layer thickness and adhesion to ensure the bottle meets the customer's specifications.
A case in point is a customized multi-layer PET line for a cosmetics brand. The brand needed a premium bottle with strict aesthetic standards and reliable barrier performance. Leshan designed a custom extrusion head that increased production efficiency by 30 percent while maintaining the required appearance. The head delivered uniform layer distribution, smooth surface finish, and consistent wall thickness. The project demonstrated how customized extrusion head design can solve both technical and commercial challenges.
Integration with Blow Molding Systems and Auxiliary Equipment
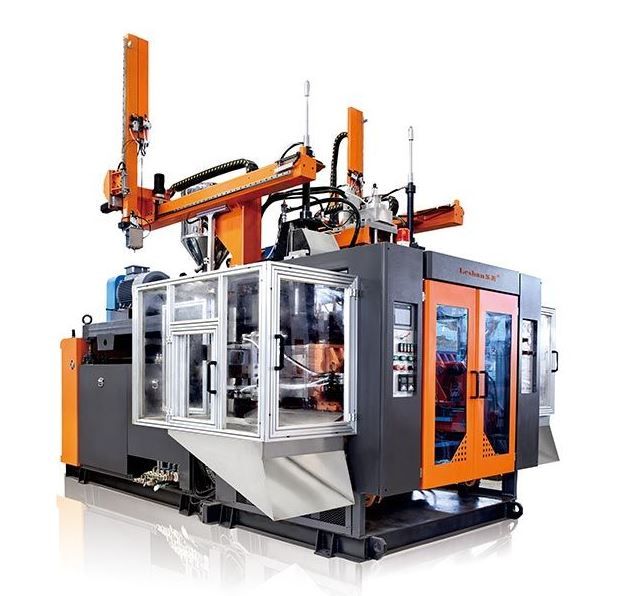
A customized extrusion head does not operate alone. It is part of a complete blow molding system. Leshan's blow molding machines are available in semi-automatic, fully automatic, or multi-station models to meet different production needs. They provide precise control of pressure and temperature, ensuring consistent quality. They support high output designs for large-scale production. They are compatible with various molds for different bottle specifications. The extrusion head must match the machine's extruder capacity, clamping force, and control architecture.
The central feeding system is another important integration point. It centrally controls the conveying and drying of plastic materials. It ensures stable temperature and reduces manual labor. It can connect multiple extruders or blow molding machines for centralized management. Its high automation reduces labor costs. Its efficient conveying minimizes material waste. It is compatible with multiple plastic types, including PET, PP, and PE. When a custom extrusion head is installed, the feeding system must deliver material at the right rate, temperature, and moisture level. Leshan's engineers coordinate these parameters during commissioning.
Auxiliary equipment also plays a role. Crushers recycle scrap and edge materials by crushing them. Mixers evenly mix different colors or functional plastic pellets. Chillers and cooling systems maintain mold and product temperature, ensuring precision. Conveyor belts automatically transport finished products for continuous production. These auxiliary systems improve production line efficiency and product quality. They reduce complexity and maintenance costs. When integrated properly with the extrusion head, they create a seamless production flow from raw material to finished bottle.
How Auxiliary Equipment Supports Extrusion Head Performance
- Crusher: Recycles scrap, reducing material waste and cost.
- Mixer: Ensures consistent color and additive distribution.
- Chiller: Stabilizes mold temperature for accurate wall thickness.
- Conveyor belt: Maintains continuous production and reduces manual handling.
- Central feeding: Delivers dry, temperature-stable material to the extruder.
Quality Control and Compliance
Quality is non-negotiable in extrusion blow molding. Leshan's products meet ISO 9001 and CE standards, ensuring safety and reliability. The factory uses continuous monitoring with visual inspection and leak-testing systems to guarantee defect rates under 0.5 percent. These quality systems apply to the extrusion head as well. During manufacturing, every critical dimension is measured and recorded. During assembly, every heater and thermocouple is tested. During trial production, every bottle is inspected for wall thickness, weight, dimensions, and appearance.
Compliance also means meeting customer-specific standards. Some customers require food-grade materials. Some require pharmaceutical cleanliness. Some require chemical resistance. Leshan's engineers select materials and finishes that satisfy these requirements. They provide documentation for material certificates, test reports, and compliance declarations. This transparency builds trust and simplifies the customer's own regulatory approvals.
Case Studies: Custom Extrusion Head Success Stories
Case Study 1: Beverage Bottle Line with Zero Mold Failure
Leshan partnered with a leading beverage company to produce over 50 million bottles annually. The project required a high-speed extrusion blow molding line with a customized extrusion head. The head needed to deliver uniform wall thickness at high output, maintain bottle strength, and resist wear from continuous operation. Leshan's engineers designed a balanced flow channel, selected high-grade steel, and integrated advanced cooling. The line achieved the target output, and the mold ran for two consecutive years with zero mold failure. This case demonstrates how precision design and durable materials can deliver long-term reliability.
Case Study 2: Multi-Layer PET Line for a Cosmetics Brand
A cosmetics brand needed a multi-layer PET bottle with a premium look and strict barrier properties. The bottle capacity was within the 100 mL to 10 L range, and the design required a specific neck finish and wall thickness. Leshan customized a multi-layer extrusion head with separate flow channels and precise layer control. The head increased production efficiency by 30 percent while maintaining strict aesthetic standards. The customer benefited from faster cycles, lower scrap, and a product that met the market's quality expectations.
Case Study 3: Industrial Container Line Running 24/7
An industrial container manufacturer required a line that could run 24 hours a day, 7 days a week. The containers were large, and the parison needed to be strong and consistent. Leshan supplied a customized accumulator head and a fully automatic blow molding system. The line ran for 18 months with minimal maintenance interruptions. The high-grade mold steel and advanced cooling system extended mold life to 5 to 8 years under continuous production. The customer achieved return on investment in under 12 months. This case highlights the durability and cost-effectiveness of a well-designed custom extrusion head.
Efficiency, Productivity, and Cost Management
Custom extrusion head design directly affects efficiency and productivity. A well-designed head reduces cycle time by improving melt flow and cooling. It reduces scrap by ensuring uniform wall thickness. It increases output by supporting higher extrusion rates. Leshan's fully automated production lines reduce labor by up to 40 percent. Multi-station blow molding machines achieve production speeds of 2,000 to 5,000 bottles per hour per station. Central feeding systems reduce material loss by 15 to 20 percent and ensure uniform drying for better product consistency.
Cost management is not only about speed. It is also about material usage, energy consumption, and maintenance. A customized extrusion head can reduce material usage by optimizing wall thickness. It can reduce energy consumption by improving heating efficiency. It can reduce maintenance costs by using durable materials and accessible designs. Auxiliary systems such as crushers, mixers, chillers, and conveyors integrate seamlessly, reducing maintenance costs by 20 percent. These savings accumulate over the life of the machine and improve the customer's profitability.
Efficiency Gains from Custom Extrusion Heads
- Faster cycle times due to optimized flow and cooling.
- Lower scrap rates due to uniform wall thickness.
- Higher output due to balanced melt distribution.
- Reduced labor due to automation and quick mold changes.
- Lower material loss due to precise parison control.
- Less downtime due to durable components and easy maintenance.
Durability, Maintenance, and ROI
Durability is a major consideration in extrusion head design. The head operates under high temperature and pressure for long periods. It must resist wear, corrosion, and thermal fatigue. Leshan uses high-grade mold steel and advanced cooling systems to extend mold life to 5 to 8 years under continuous production. The extrusion head is designed with replaceable components where possible, so that worn parts can be changed without replacing the entire assembly. This design philosophy reduces long-term costs and improves return on investment.
Maintenance is also simplified. The engineers consider access when designing the head. They place heating elements, thermocouples, and fasteners in locations that are easy to reach. They provide clear documentation and training. They recommend preventive maintenance schedules that include cleaning, inspection, and replacement of wear parts. When maintenance is planned and efficient, unplanned downtime is minimized. The industrial container case showed that a well-maintained line can run 24/7 for 18 months with minimal interruptions.
Customer-Centric Project Management
Managing customized extrusion head designs is as much about project management as it is about engineering. Leshan uses a structured process to keep projects on track. The process includes clear milestones, regular communication, and documentation. The customer knows what to expect at each stage. The factory knows what is required to deliver on time. This transparency reduces risk and builds trust.
The customer-centric approach means listening, adapting, and delivering solutions that work best for the customer. If the customer's needs change during the project, the factory adjusts. If a technical challenge arises, the engineers collaborate to solve it. If a deadline is tight, the project team prioritizes critical tasks. This flexibility is a core reason why businesses choose Leshan. The company does not believe in one-size-fits-all solutions. Every project is customized to meet unique production needs.
Common Challenges and How the Factory Overcomes Them
Custom extrusion head projects often face challenges. One challenge is balancing performance with cost. A highly optimized head may be expensive to manufacture. Leshan addresses this by using modular design and standardized components where possible. This approach reduces cost without sacrificing quality. Another challenge is material variability. Different batches of resin can behave differently. The factory overcomes this by testing materials and designing heads with adjustable parameters. Another challenge is integration with existing equipment. Leshan's engineers review the customer's line and design the head to fit. They also provide on-site support during installation.
Time pressure is another common challenge. Customers want fast delivery without compromising quality. Leshan uses efficient project management, advanced manufacturing, and simulation to shorten lead times. The quick mold-change system minimizes downtime to under 10 minutes, allowing fast production adaptation. This speed is a competitive advantage for customers who need to respond to changing market demands.
Future Trends in Custom Extrusion Head Design
The future of extrusion blow molding is shaped by sustainability, digitalization, and automation. Customers are increasingly using recycled materials, which can be more challenging to process. Custom extrusion heads must handle these materials without compromising quality. They must also support lightweighting, which reduces material usage and carbon footprint. Digitalization is another trend. Sensors and data analytics can monitor extrusion head performance in real time. Predictive maintenance can prevent failures before they occur. Automation can adjust parameters automatically to maintain optimal conditions.
Leshan continuously improves and optimizes its products to stay ahead of industry advancements. The company invests in research and development, adopts new manufacturing technologies, and listens to customer feedback. These efforts ensure that customized extrusion head designs remain at the forefront of the industry. As the market demands more complex bottles, more sustainable materials, and higher efficiency, the factory's ability to manage customization will become even more important.
Conclusion: Customization as a Strategic Advantage
Managing customized extrusion head designs is a complex but rewarding capability. It requires technical expertise, precision manufacturing, project management, and customer collaboration. Factories that excel at it can deliver blow molding systems that produce better bottles, faster, and at lower cost. Leshan, with over 15 years of experience, has developed a structured approach to customization. From requirement gathering and material assessment to design simulation, precision machining, testing, installation, and lifecycle support, every step is designed to ensure success.
The company's key offerings, including blow molding systems, centralized feeding systems, fully automatic systems, customized project solutions, and comprehensive support, all contribute to this success. Its blow molds, central feeding systems, auxiliary equipment, and blow molding machines work together to create seamless production lines. Its core advantages, such as proven expertise, tailored solutions, reliability, customer-centric approach, and innovative technology, make it a trusted partner. For businesses that need customized extrusion heads, working with a factory like Leshan can be a strategic advantage. It means access to precision engineering, durable equipment, efficient production, and long-term support. It means a partnership that focuses on success, not just a transaction.
In the end, the extrusion head is more than a component. It is the heart of the blow molding process. How a factory manages its customization determines the quality, efficiency, and profitability of the entire production line. Leshan's approach shows that with the right expertise, processes, and commitment, customized extrusion head designs can be managed successfully, project after project.